Case Study: Reducing Flash-Related Rejection Rate Below 0.5% in a 64-Cavity Cap Mold
Case Study: Reducing Flash-Related Rejection Rate Below 0.5% in a 64-Cavity Cap Mold
Published by cap-molds — China's Leading Precision Bottle Cap Mold Manufacturer & High-Cavitation Closure Tooling Specialist
Executive Summary: Solving Flash Defects in High-Density Tooling
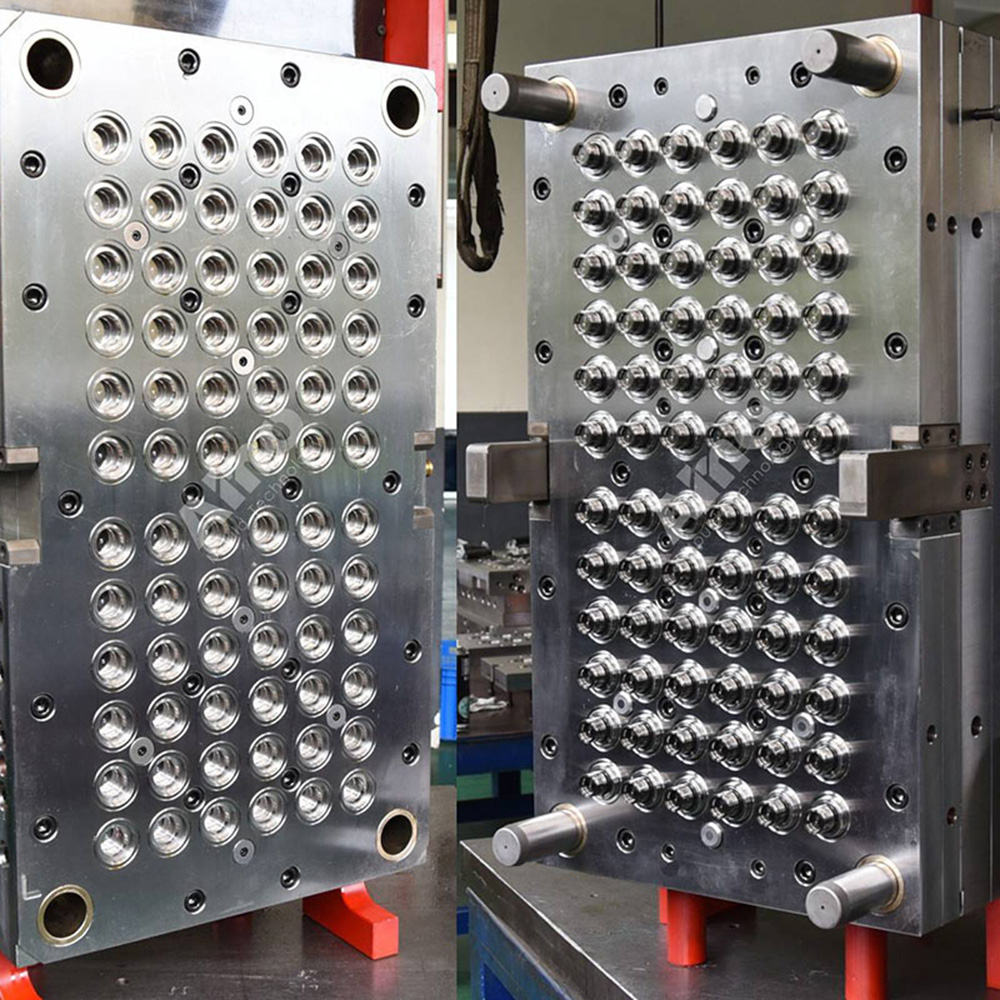
In high-speed beverage closure manufacturing, flash defects are a primary cause of quality rejections, unexpected machine downtime, and premature tool wear. A multinational bottling company approached cap-molds after experiencing unacceptable flash-related rejection rates exceeding 4.2% on a competitor's 64-cavity water cap mold. The flash was severely compromising tamper-evident band integrity and creating automated capping line jams.
By re-engineering the cavity stack architecture, optimizing parting line micro-flatness within 0.008mm, and balancing hot runner thermal zones, cap-molds successfully lowered the client's flash-related rejection rate to below 0.35% while simultaneously reducing dry cycle time to 2.3 seconds.
1. Initial Audit & Root Cause Analysis
Our engineering team conducted a comprehensive teardown and dynamic Moldflow analysis of the client's existing 64-cavity tooling system. Diagnostic evaluations identified three structural factors driving the high defect rate:
- Platen & Plate Deflection: Insufficient mold base support pillars caused 0.022mm flexing across the center cavities under 400-ton clamping force, opening parting lines during peak packing pressure.
- Manifold Thermal Imbalance: Temperature variances up to ±4.8°C across outer and inner nozzle drops caused severe resin viscosity drops in hotter zones, forcing melt into shut-off clearances.
- Stripper Ring Wear & Misalignment: Core pin eccentricity exceeded 0.006mm, causing uneven friction and premature gapping along the stripper plate shut-off interface.
2. Tooling Redesign & Engineering Breakthroughs by cap-molds
To eliminate systemic flash, cap-molds replaced the flawed core-cavity stacks and mold base structure with our proprietary ultra-precision closure tooling design.
| Engineering Vector | Legacy Tooling Configuration | cap-molds Precision Engineering Solution |
|---|---|---|
| Parting Line Flatness | ±0.020mm (Manual fitting) | Sub-micron optical surface grinding achieving flatness within 0.008mm across all 64 cavities |
| Steel Metallurgy | Standard pre-hardened tool steel | Hardened ESR Stainless Steel (S136 / Stavax ESR, HRC 52-54) for maximum shut-off wear resistance |
| Hot Runner System | Global thermal zones | Direct needle valve gate system featuring individual closed-loop PID thermal control per drop (±0.3°C precision) |
| Core Centering | Conventional sliding fit | Self-centering dual-taper core alignment geometry preventing core shift under 1,200 bar injection pressure |
3. Empirical Validation and Field Performance Results
Following full assembly and cleanroom testing at the cap-molds facility, the re-engineered 64-cavity cap mold underwent a continuous 120-hour production run using food-grade Organoleptic HDPE resin.
- Rejection Rate Collapse: Automated inline vision inspection systems verified a flash-related rejection rate reduction from 4.2% down to 0.32% over 2,500,000 continuous shots.
- Enhanced Weight Consistency: Cavity-to-cavity cap weight variance was locked within ±0.007g, eliminating localized over-packing.
- Cycle Time Optimization: Beryllium Copper (BeCu) conformal core inserts accelerated gate-area heat evacuation, reducing cycle time from 2.8s to 2.3s.
- Zero Parting Line Crush: Uniform shut-off force distribution prevented steel hobbing, ensuring long-term mold maintenance intervals beyond 5 million cycles.
4. Strategic Key Takeaways for Closure Converters
Achieving stable, flash-free production in multi-cavity cap molds requires moving away from manual bench fitting toward absolute digital machining tolerances. Combining sub-10-micron parting line flatness with balanced thermal distribution ensures maximum production uptime, reduced resin waste, and lower operational unit costs.
Partner with cap-molds for Flash-Free Closure Tooling
At cap-molds, we specialize in high-cavitation plastic cap molds engineered for demanding packaging applications. Whether you require a 32, 48, 64, or 96-cavity closure tool, our technical team delivers fully customized, zero-defect solutions tailored to your exact bottle neck finishes.