Case Study: Supporting a Beverage Manufacturer's Cap Line Expansion in Southeast Asia
Rapid urbanization, a growing young demographic, and strong seasonal demand for bottled water, ready-to-drink (RTD) beverages, sports drinks, and carbonated soft drinks (CSDs) continue to drive heavy capital investment across Southeast Asia's beverage packaging sector. For regional bottlers and closure converters expanding production capacity, scaling output is no longer just about adding extra molding presses—it requires high-cavitation tooling engineered for sub-four-second cycle times, regulatory neck/closure compatibility, consistent tamper-evident (TE) band performance, and reliable operation under hot, humid ambient conditions.
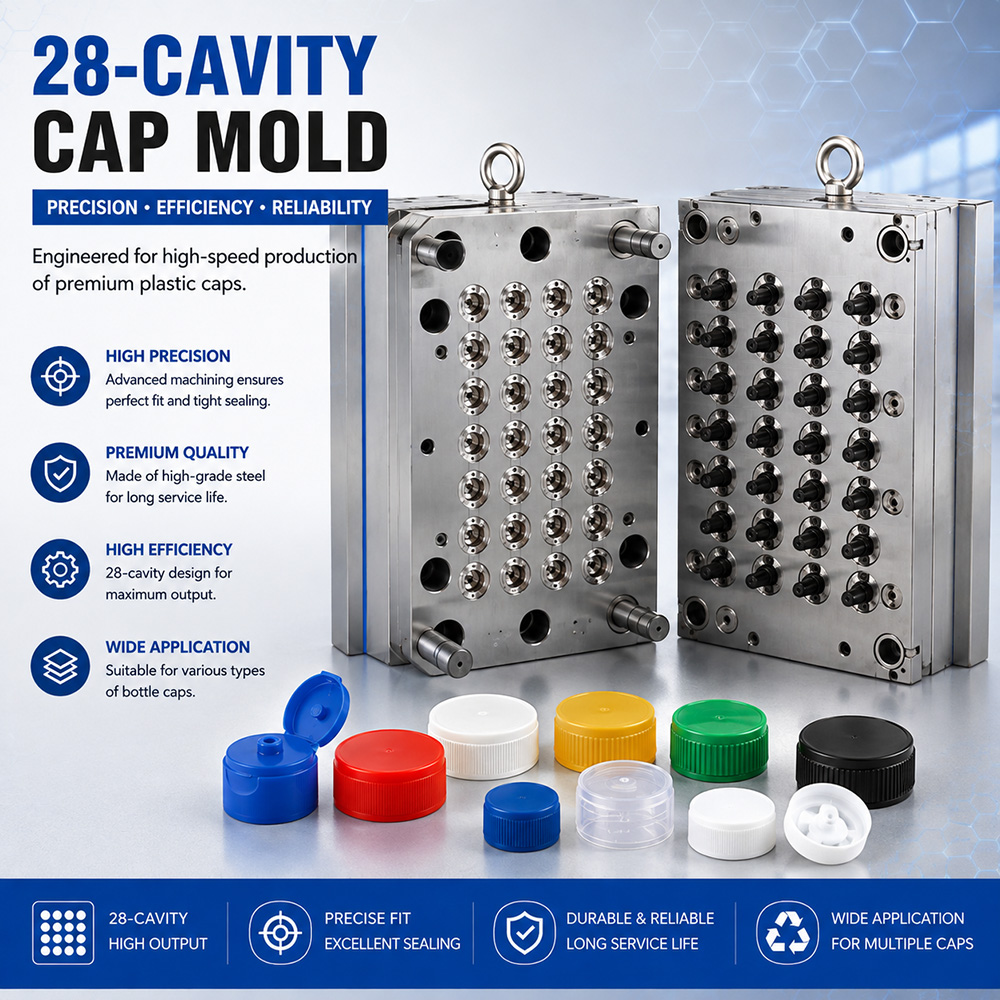
As a specialized Chinese bottle cap mold manufacturer and turnkey closure tooling solution expert, cap-molds partnered with a high-growth Southeast Asian beverage manufacturer to execute a multi-mold closure line expansion. This technical case study details the engineering bottlenecks addressed, the precision tooling architecture deployed, and the operational results achieved across the client's expanded production floor.
1. Expansion Challenges in a High-Growth Southeast Asian Bottling Plant
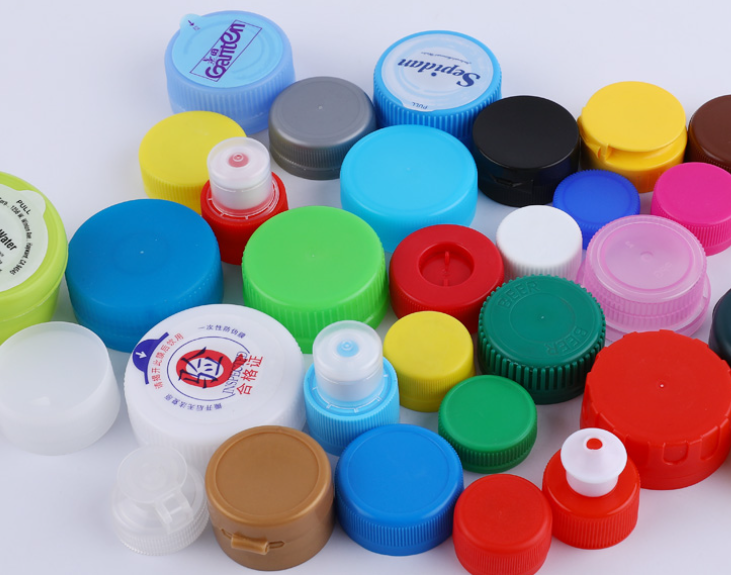
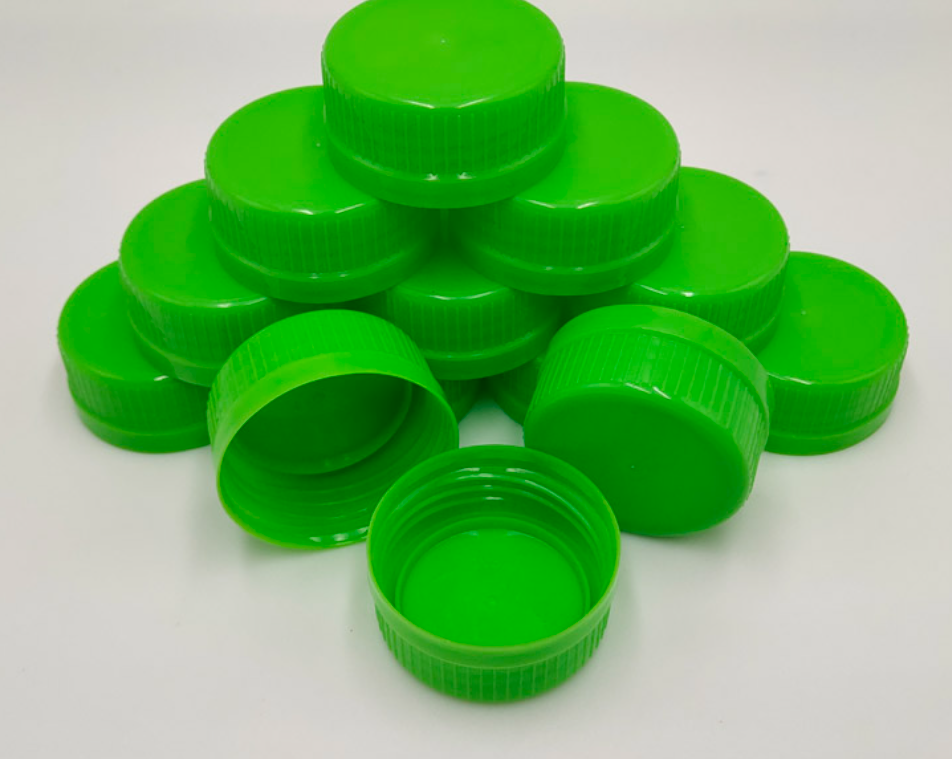
To support surging regional distribution across both still water and carbonated beverage lines, the client needed to increase in-house closure manufacturing capacity for 29/25 lightweight still water caps and PCO 1881 CSD closures while preparing for evolving regional sustainability and tethered-closure specifications. An engineering review by cap-molds identified four primary operational bottlenecks on their existing setup:
- Cycle Time & Cavitation Limits: Older 36- and 48-cavity molds suffered from non-uniform cooling near outer cavity rows and prolonged cycle times (above 5.0 seconds), restricting hourly output per press during peak demand seasons.
- High Ambient Humidity & Condensation Risks: Elevated plant humidity across tropical Southeast Asian facilities increases condensation risk on chilled mold surfaces, requiring corrosion-resistant steels and tight thermal sealing to protect parting lines and prevent moisture-related defects.
- Tamper-Evident (TE) Band Integrity & Stripper Wear: High-speed stripping of thin-walled HDPE and PP closures frequently caused TE bridge tearing or inconsistent hinge/band formation when core/cavity clearances and cooling rates were not tightly synchronized.
- Maintenance Downtime & Changeover Delays: Extended mold removal and teardown times for routine wear-part service reduced Overall Equipment Effectiveness (OEE) and strained local maintenance resources.
2. Precision Tooling & Process Solutions by cap-molds
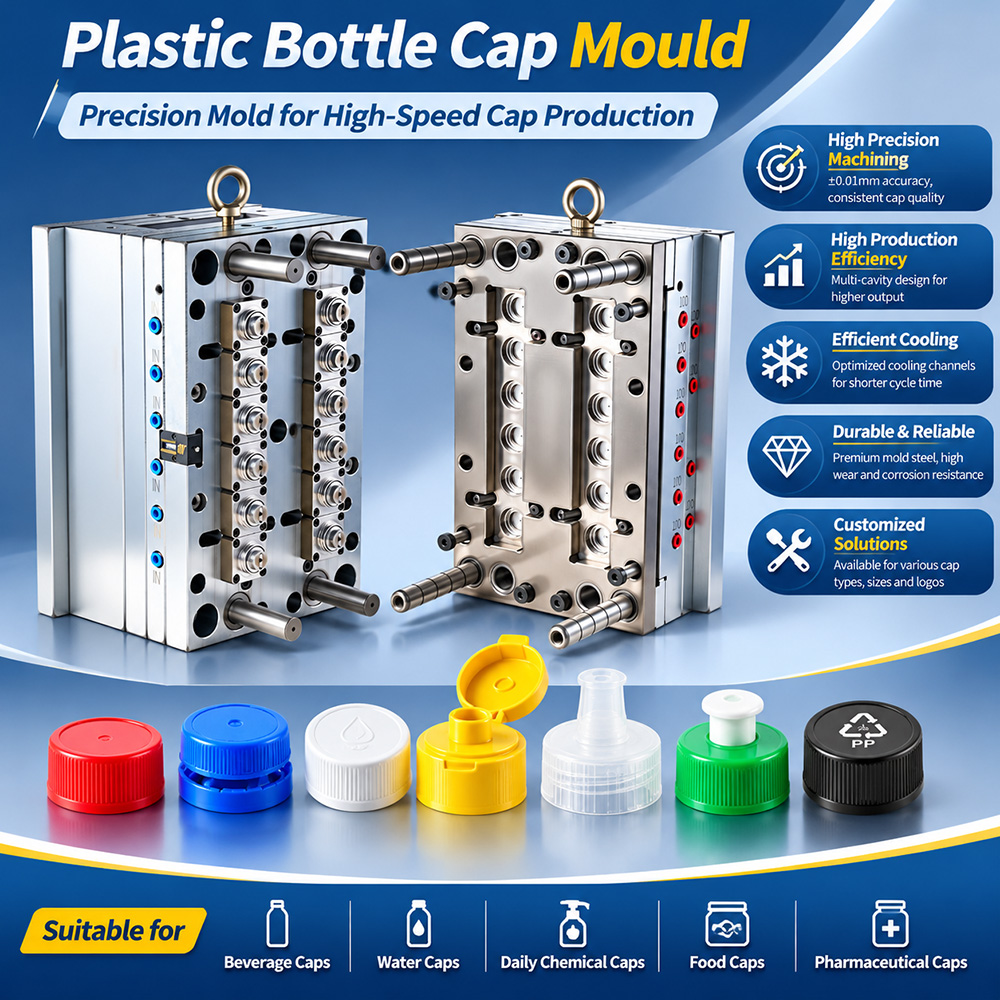
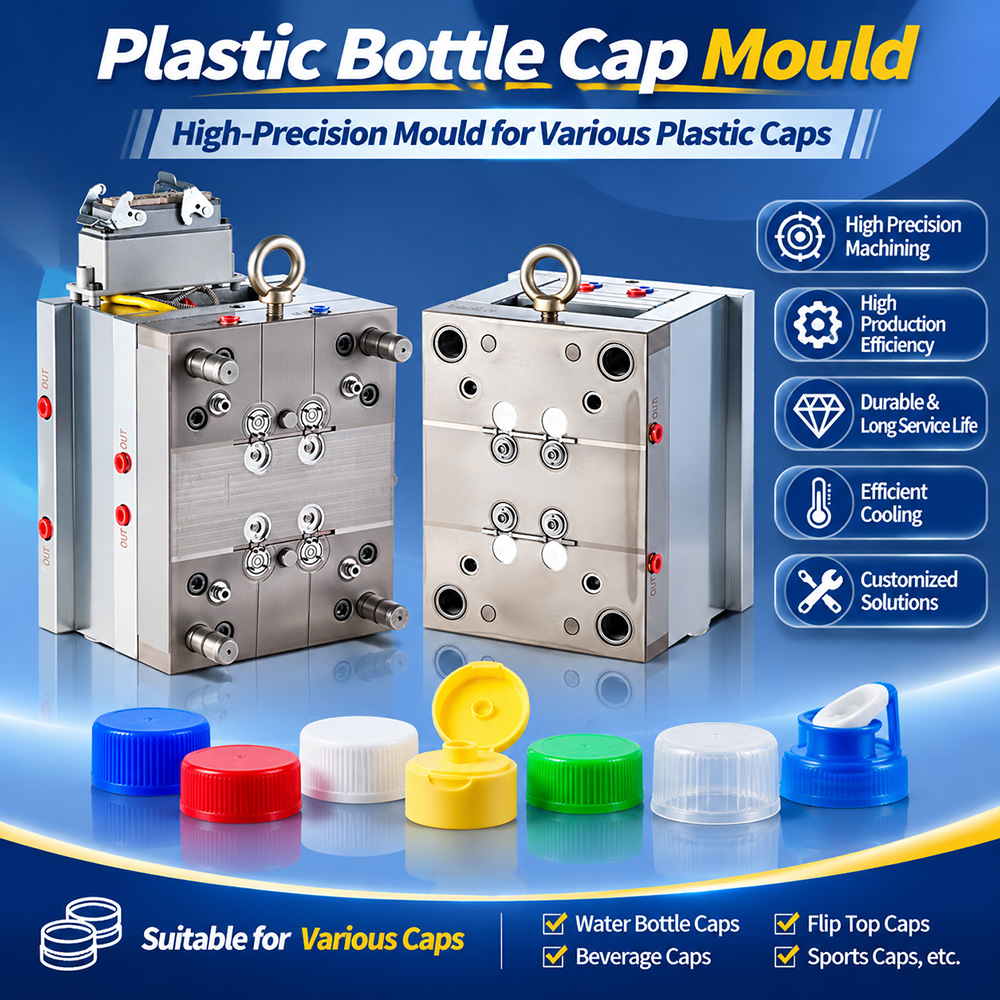
To deliver dependable, high-speed closure output without compromising dimensional accuracy or drop-test/seal performance, cap-molds engineered high-cavitation injection cap molds tailored to the client's press tonnage, resin grades, and downstream capping equipment:
A. Naturally Balanced Hot Runner & Gate-Zone Thermal Control
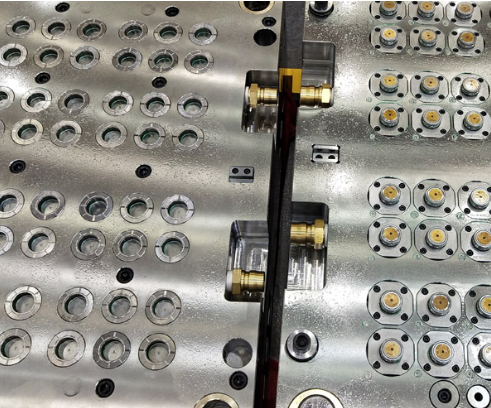
cap-molds designed a rheologically balanced hot runner system with multi-zone temperature control to maintain uniform melt viscosity and flow balance across every cavity. Balanced filling minimizes internal residual stress, prevents gate blush or stringing, and ensures uniform cap weight and wall distribution from shot to shot.
B. High-Efficiency Cooling Circuits & Corrosion-Resistant Metallurgy
Because cooling dominates closure molding cycle times, cap-molds integrated precision-positioned cooling channels around the core, cavity, and neck-ring/TE-band zones to accelerate heat extraction and stabilize shrinkage. Key sliding and molding surfaces were machined from hardened, corrosion-resistant stainless steel grades and precision-finished to maintain tight concentricity, smooth release, and resistance to humid plant conditions.
C. Modular Wear Components & Synchronized Ejection
To support continuous multi-shift operation and simplify routine servicing, cap-molds incorporated modular, interchangeable wear inserts and precision alignment components. Controlled stripper-plate and ejection kinematics ensured clean, distortion-free release of tamper-evident bands and threaded or tethered cap geometries at high cycling speeds.
3. Expansion Performance Summary
Following factory acceptance trials, dimensional inspection, and line integration support from cap-molds, the client's expanded closure line achieved substantial gains in throughput, consistency, and maintenance efficiency:
| Performance & Tooling Metric | Prior Baseline Setup | cap-molds Expansion Solution | Operational Impact |
|---|---|---|---|
| Cavity Architecture | 36 – 48 Cavities | High-Cavity Precision Cap Molds (up to 72+ Cavities) | Higher output per injection press |
| Cycle Time | > 5.0 seconds | Sub-4.0 second high-speed cycle capability | Significant increase in hourly cap yield |
| Cavity-to-Cavity Consistency | Noticeable weight & cooling drift | Balanced hot runner & uniform cooling | Tighter cap weight & dimensional stability |
| Corrosion & Wear Protection | Standard tooling prone to humidity wear | Corrosion-resistant steel & modular wear parts | Reliable tropical operation & faster servicing |
4. Conclusion: Partnering with cap-molds for Regional Closure Growth
Scaling a beverage closure line in Southeast Asia requires more than high cavity counts—it demands precision thermal engineering, balanced hot runner flow, reliable tamper-evident band demolding, and service-friendly mold construction built for continuous production.
As a dedicated Chinese manufacturer of bottle cap molds and complete closure tooling solutions, cap-molds supports beverage, water, CSD, dairy, and packaging converters worldwide with custom-engineered molds, DFM/Moldflow analysis, and thorough pre-shipment testing. Contact the cap-molds engineering team today to discuss your next cap line expansion or custom closure tooling project.